
Search history
Clear allSearch by image
XDrag and drop an image here or upload an image
Max 5MB per image
UploadSign In | Join
Search history
Clear allSearch by image
XDrag and drop an image here or upload an image
Max 5MB per image
UploadSign In | Join
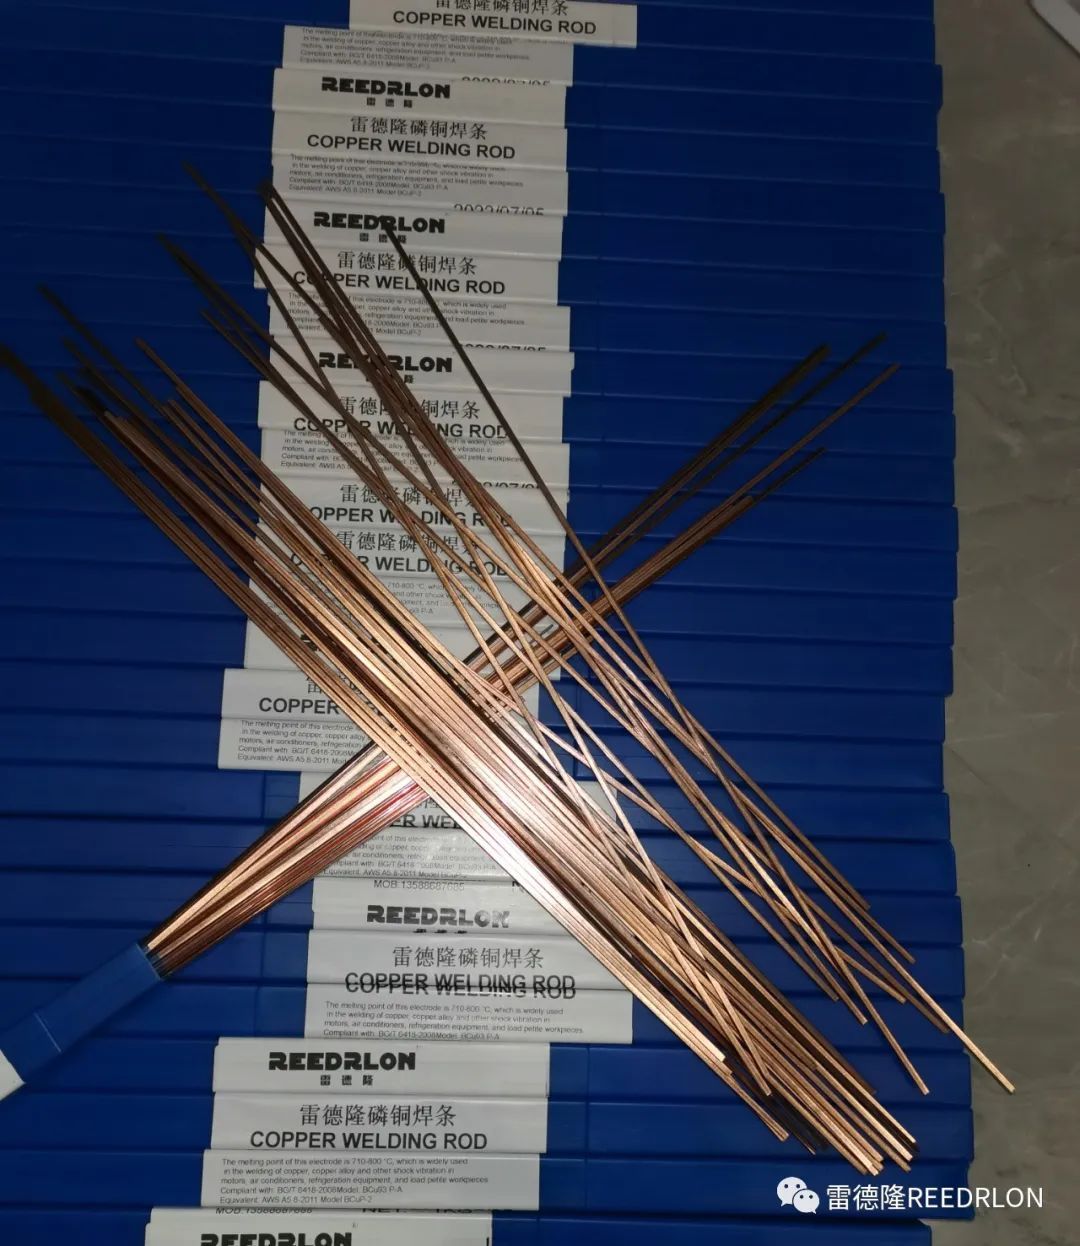
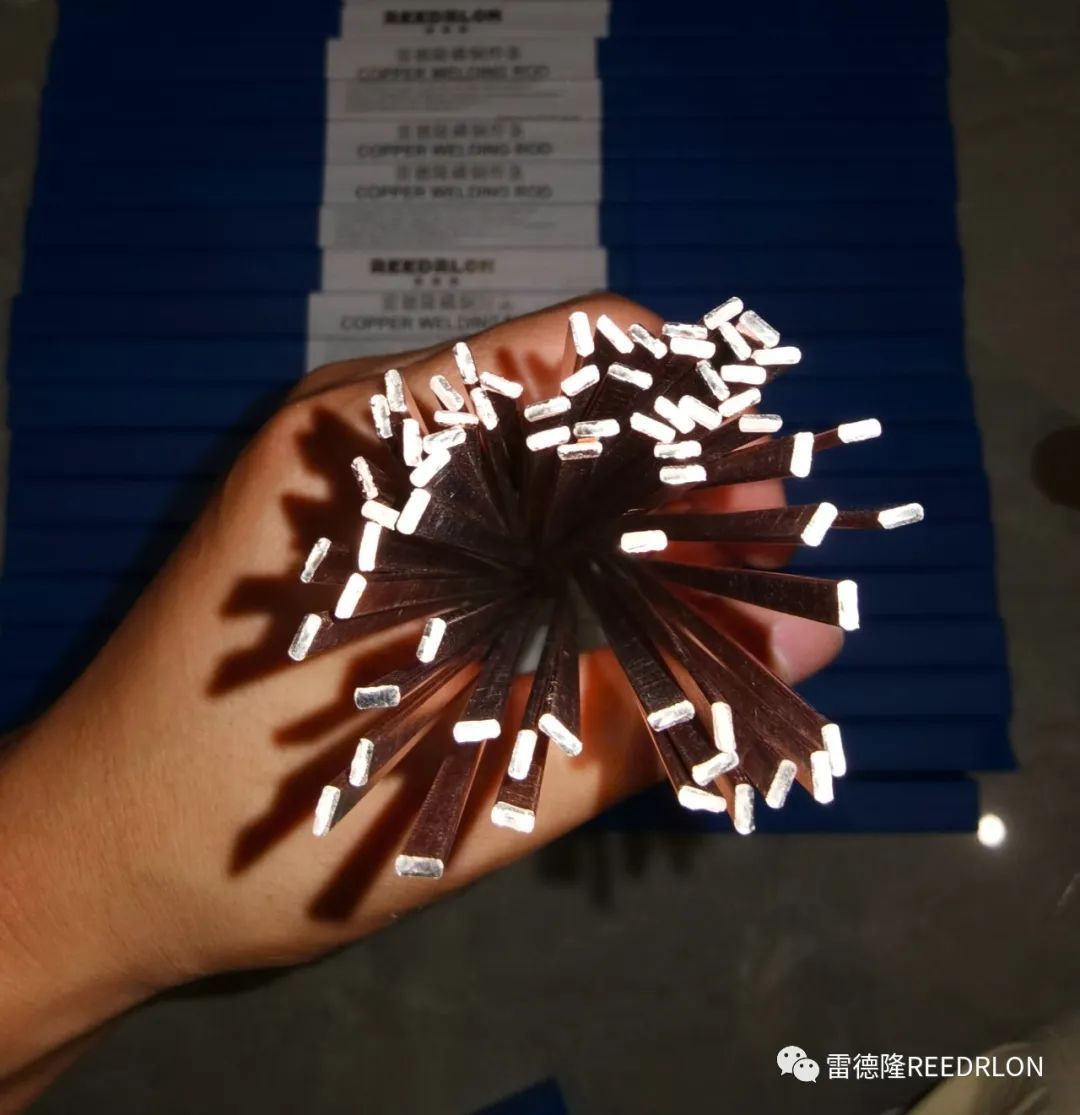
thicknessthickness)1.3 mm
Length (Length)400mm 500mm
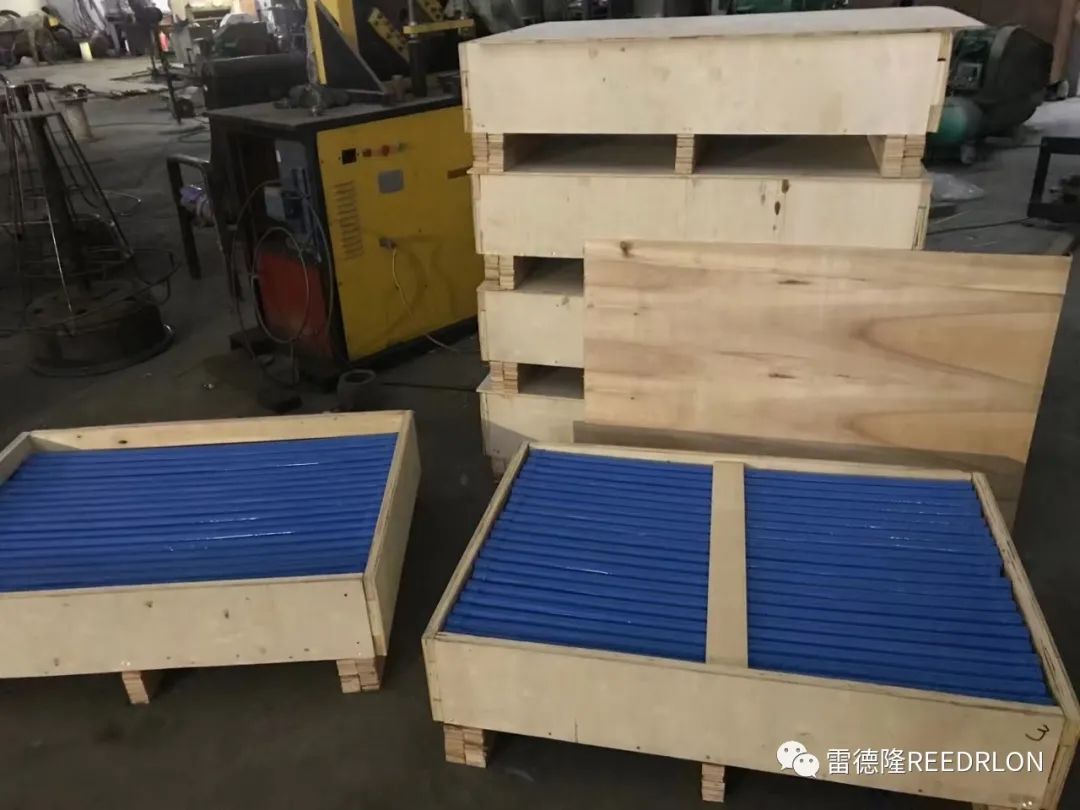
PackagingPacking)1 kg/box
Welding of copper and copper pipe fittings for the refrigeration systems of air conditioners, chillers, and refrigerators
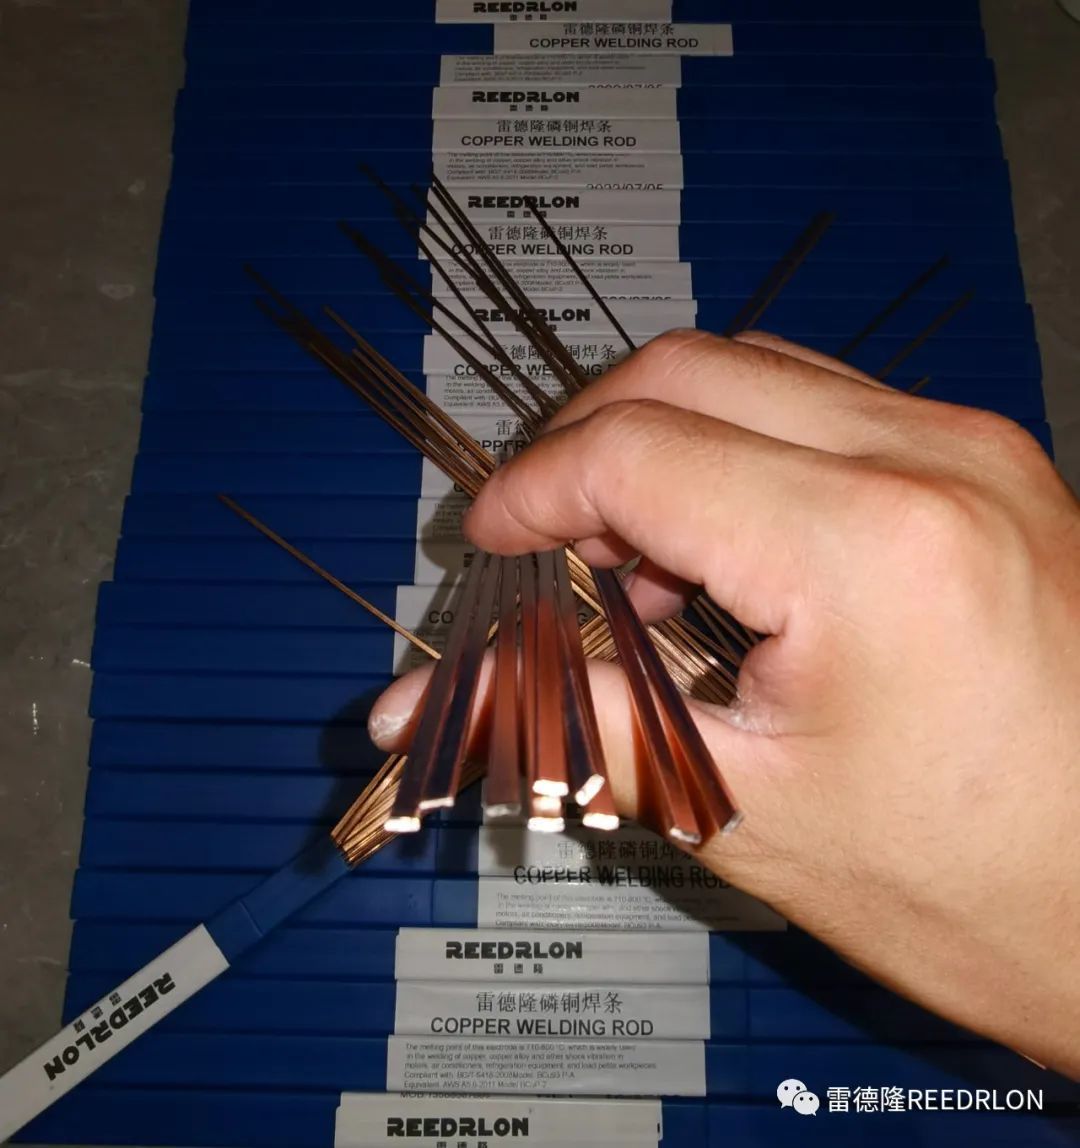
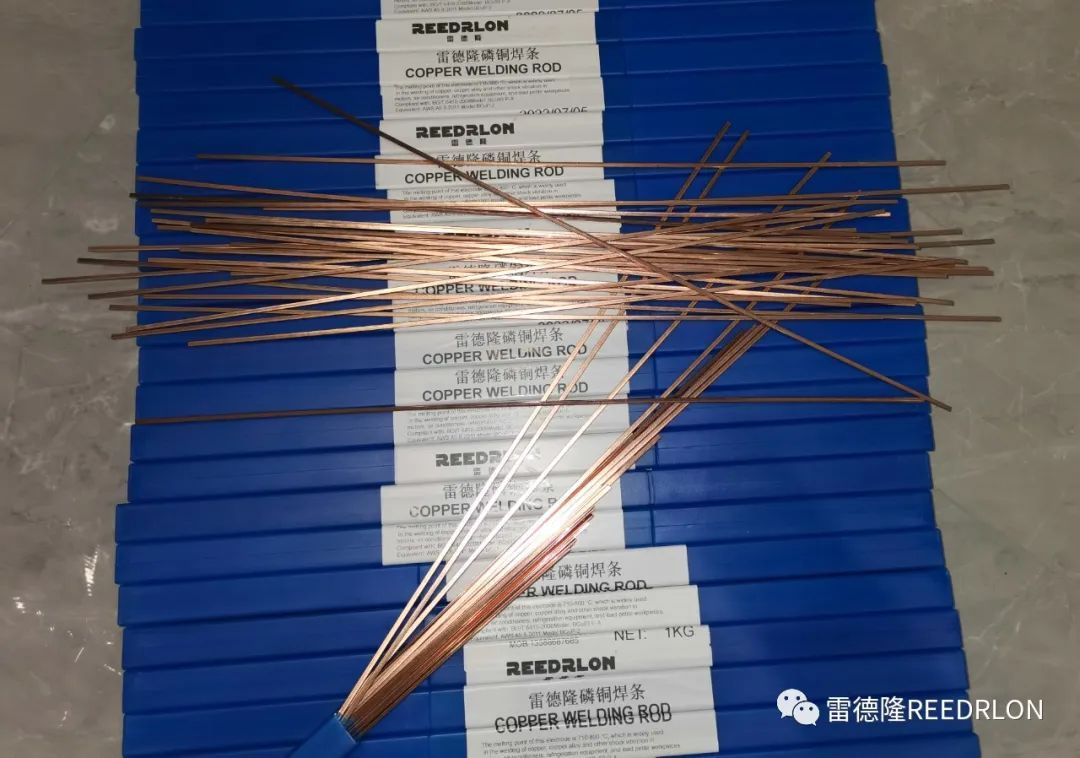
Phosphorus-copper welding rods, suitable for welding copper-to-copper pipe connections in the refrigeration systems of air conditioners, refrigerators, and freezers.
Used for welding copper and copper pipe joints in the refrigeration systems of air conditioners, freezers, and refrigerators
Phosphor COPPER electrode, suitable for welding copper and copper pipe joints in the refrigeration system of air conditioners, freezers, and refrigerators.
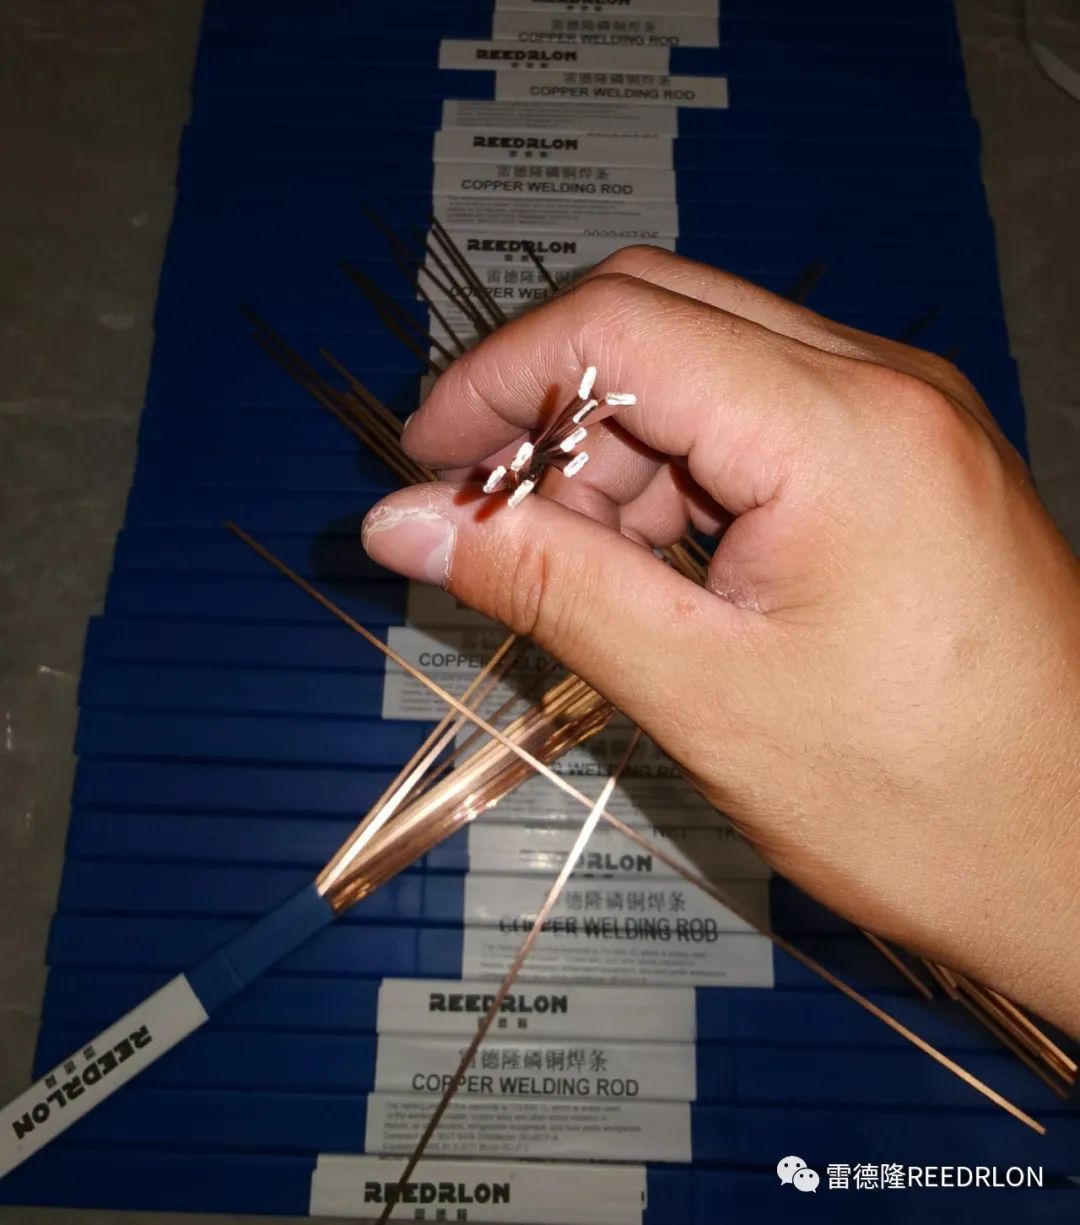
Chinese Name: Phosphorus Copper Welding Electrodes
Chemical composition:P:6.8-7.2
Use Route: Air conditioners, refrigerators
Sex Capability: Low melting point, good fluidity
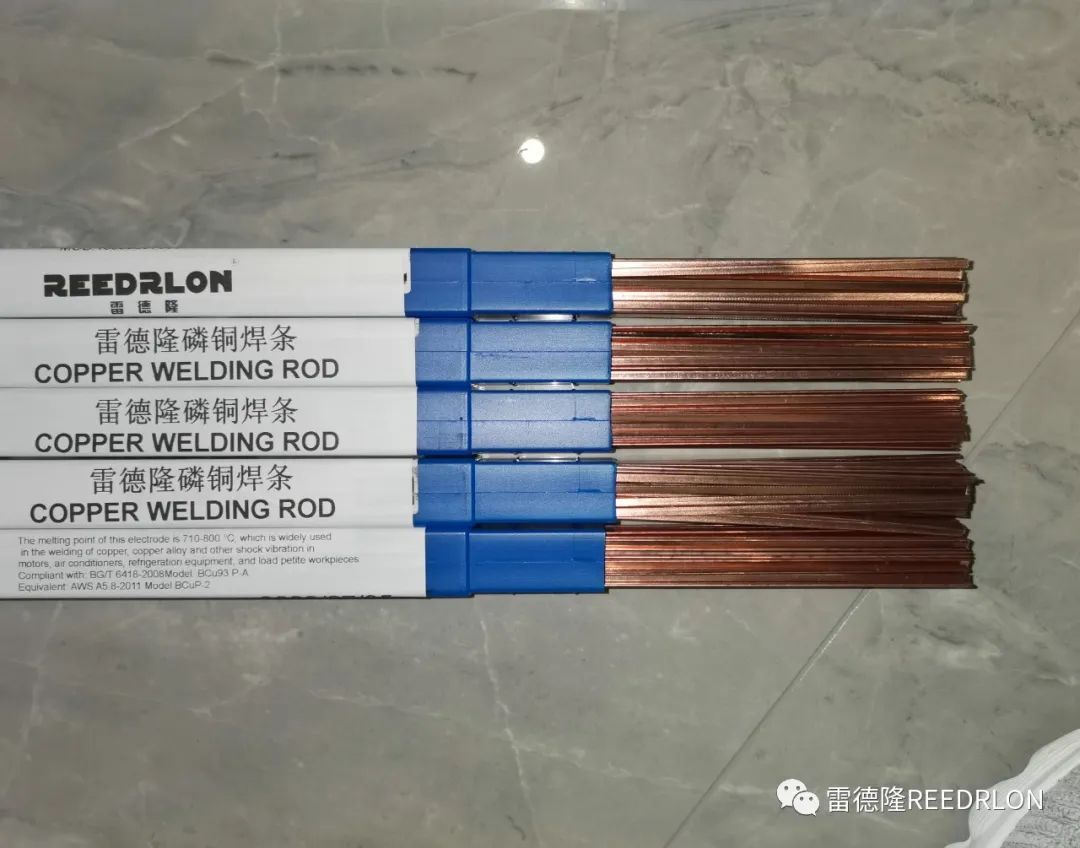
Chinese name
Phosphorus copper electrode
Chemical composition
P: 6.8 to 7.2
In the manner of
Air conditioner, freezer
Sex can
Low melting point and good fluidity
Editor Broadcast
Phosphorus copper welding rod:BCU93P,BCU91PAG
Main,Cu:margin
Editor Broadcast
Welding Temperature710-810℃, low melting point, good fluidity, low cost, silver-saving, alternative silver.
Editor Broadcast
1,BCu92P: IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>7.5-8.5%, Copper: Remaining amount. Melting temperature710-750℃, with a low melting point, this solder has good fluidity but is brittle. It is typically used for brazing copper and brass parts that are not subjected to impact loads or vibration;
2,BCu93P(HL201/BCuP-2) : IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>6.80-7.50%, Copper: Remaining amount. Melting temperature710-793℃<t_XXXXX>the solder has good fluidity and can flow into joints with very small gaps, but the brazing material is brittle and is generally used in the mechanical and instrumentation industries for copper and brass parts that are not subjected to impact loads;</t_XXXXX>
3,BCu89SnP(HL208) : IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>6.80-7.50%, Tin:5.0-6.0%, Copper: Remaining amount. Melting temperature620-660℃<t_ melting point> has a low melting point and good fluidity, allowing brazing with silver flux for copper, brass, bronze, and low-zinc brass parts;
4,BCu86SnP: IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>4.80-5.80%, Tin:7.00-8.00%, Nickel:0.40-1.20%, Copper: Remaining amount. Melting temperature620-670℃, the use of this solder is the same as before. The addition of nickel increases brittleness, but improves fluidity, and the weld is shiny. It is generally used for copper and brass brazing.
5,BCu91AgP(HL209/BCuP-6) : IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>5.50-7.50%, silver1.80-2.20%, Copper: Remaining amount. Melting temperature645-771℃, with a low melting point, this solder can fill joint gaps over a wide temperature range. It is commonly used for brazing copper and brass parts in industries such as refrigerators, air conditioners, motors, and instruments;
6,BCu89AgP(BCuP-3) : IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>5.8-6.70%, silver4.80-5.20%, Copper: Remaining amount. Melting temperature645-788℃, with a low melting point, this solder exhibits improved ductility and electrical conductivity, though its fluidity is moderate. It is suitable for brazing copper and brass parts with larger gaps.
7,BCu88AgP(HL205/BCuP-7) : IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>6.50-7.00%, silver4.80-5.20%, Copper: Remaining amount. Melting temperature645-780℃, with a low melting point, this solder exhibits improved ductility and electrical conductivity, and its fluidity is betterB-Cu89PAg, generally used for copper and brass parts with large brazing gaps;
8,BCu87PAg(BCuP-4) : IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>7.0-7.5%, silver5.80-6.20%, Copper: Remaining amount. Melting temperature645-718℃, with a low melting point, this solder has excellent fluidity and can be used for brazing joints with small gaps. It is generally used for brazing copper and brass components;
9,BCu80PAg(HL204/BCuP-5) : IngredientsP<t_XXXXXXXXX> <t_XXXXXXXXX>4.80-5.30%, silver1.4.50-1.5%, Copper: Remaining amount. Melting temperature645-815℃, with a low melting point, the ductility and electrical conductivity of this solder are further improved, suitable for welding applications requiring higher standardsHL205(5%Copper and brass parts with high brazing materials and large joint gaps.
10,BCu6₀ZnSn-R(S2X1/RBCuZn-A) : Ingredient Copper:5.9.0-61.0%, tin0.80-1.20%, Silicon:0.15-0.35%, Zinc: Remaining amount. Melting temperature890-905℃<t_XXXXX>Its melting point is high, making it suitable for welding hard alloy tools, molds, and mining equipment. It can also replace existing materials.H62Welding flux used to achieve a denser weld joint, and can also serve as welding wire for gas welding brass
Introduction to the
Editors broadcast
Phosphorus copper electrode: BCU93P, BCU91PAG
Main, Cu: allowance
Performance of phosphor copper electrode
Editors broadcast
Brazing temperature: 710-810℃, low melting point, good fluidity, low cost, silver-saving, silver substitute.
Classification and Composition
Editors broadcast
1, BCu92P: composition P: 7.5-8.5%, copper: allowance. Melting temperature 710-750℃, low melting point; the solder has good fluidity, but is relatively brittle. It is generally used for brazing without impact loads, or for welding copper and brass parts without vibration;
2, BCu93P (HL201/ BCUP-2) : composition P: 6.80-7.50%, copper: allowance. Melting temperature 710-773℃; the solder fluidity is good, it can flow into the joint with a small gap, but the solder is brittle. It is generally used in the mechanical, electrical, and instrument industries for brazing copper and brass parts without impact load.
3, BCu89SnP (HL208): composition P: 6.80-7.50%, tin: 5.0-6.0%, copper: allowance. The melting temperature is 620-660℃. The solder has a low melting point and good fluidity. It can braze copper, brass, bronze, and low-zinc brass parts using a silver brazing agent.
4, BCu86SnP: composition P: 4.80-5.80%, tin: 7.00-8.00%, nickel: 0.40-1.20%, copper: allowance. Melting temperature 620-At 670℃, the soldering process is the same as above. The addition of nickel increases brittleness, but improves fluidity, resulting in a bright weld. It is generally used for brazing copper and brass.
5, BCu91AgP (HL209/ BCUP-6) : Composition P: 5.50-7.50%, silver 1.80-2.20%, copper: allowance. Melting temperature 645-771℃, low melting point; the solder can fill the joint gap across a wide temperature range, mainly used in refrigerators, air conditioners, motors, instruments, and other industries for brazing copper and brass parts;
6, BCu89AgP (BCUP-3): composition: P: 5.8–6.7%, silver: 4.8–5.2%, copper: allowance. The melting temperature is 645-At 788℃, the melting point is low; the ductility and conductivity of the solder are improved, fluidity is good, and it is suitable for copper and brass parts with large brazing gaps.
7, BCu88AgP (HL205/ BCUP-7) : Composition P: 6.50-7.00%, silver 4.80-5.20%, copper: allowance. The melting temperature is 645-At 780°C, the melting point is low; the ductility and conductivity of the solder are improved, and its fluidity is better than B.-Cu89PAG is typically used for brazing copper and brass components with large gaps;
8, BCu87PAg (BCUP-4) : Composition P: 7.0-7.5%, silver 5.80-6.20%, copper: allowance. Melting temperature 645-718℃, low melting point; the solder has a low melting point and good fluidity, allowing brazing of joints with small gaps. It is generally used for brazing copper and brass components.
9, BCu80PAg (HL204/ BCUP-5) : composition P: 4.80-5.30%, silver 1.45-15.50%, copper: allowance. With a melting temperature of 645-815℃ and a low melting point; the ductility and electrical conductivity of the solder are further enhanced. It is used for welding copper and brass parts with a larger joint gap than the HL205 (5% silver) filler metal.
10, BCU60ZNS-R (S221/ RBCuZN-A) : Copper: 5.90-61.0%, tin 0.8-1.20%, silicon: 0.15-0.35%, zinc: specified amount. The melting temperature ranges from 890℃ to 905℃, and the solder melting point is high. It can be used for welding hard alloy tools, dies, and mining tools. It can also replace H62 solder to achieve a relatively dense weld, and can be used as gas welding brass wire.
Large quantity of in-stock items! Looking forward to working with you!
A large quantity of spot supply! Looking forward to cooperating with you!
Believe in the power of professionalism!
We take焊 rods seriously!
Please select Redron!
Redron is with you!!!
Believe in the power of professionalism!
We are committed to developing welding rods!
Good welding rod, please choose REEDRLON!
REEDRLON with you toghter! !!
Update time:


TOP


